Top 10 China Slot Die Coating Machine Manufacturers?
China’s slot-die coating equipment industry is gaining attention from battery, optical-film, solar, and flexible-electronics manufacturers. The International Energy Agency reported that global electric-vehicle battery demand exceeded 750 GWh in 2023. That growth increases pressure for uniform electrode layers, stable production speeds, and lower material waste.
A Slot Die Coating Machine can meter coating fluid directly onto a moving substrate. Its value depends on more than a polished frame. Pump accuracy, shim design, die-lip precision, web tension, drying control, and after-sales support matter equally. Edward D. Cohen, a respected coating-process author, describes slot-die coating as “a pre-metered coating process.” That short definition carries serious practical meaning. It explains why small flow changes can create visible streaks, edge beads, or uneven battery layers.
This introduction to the Top 10 China Slot Die Coating Machine Manufacturers compares technical capability, application experience, customization, quality control, and service responsiveness. Industry reports from MarketsandMarkets also connect battery-coating demand with expanding lithium-ion production and energy-storage investment. However, market forecasts are not factory guarantees. Some supplier claims remain difficult to verify publicly. That is worth admitting. A machine may look impressive during a demonstration, yet perform differently under continuous production, abrasive slurries, or strict cleanroom conditions. The following overview therefore focuses on evidence, not promotional language. It considers production examples, engineering details, certifications, and customer support. Readers should still request sample trials and measured coating data before making a purchasing decision. Small details often decide large projects.
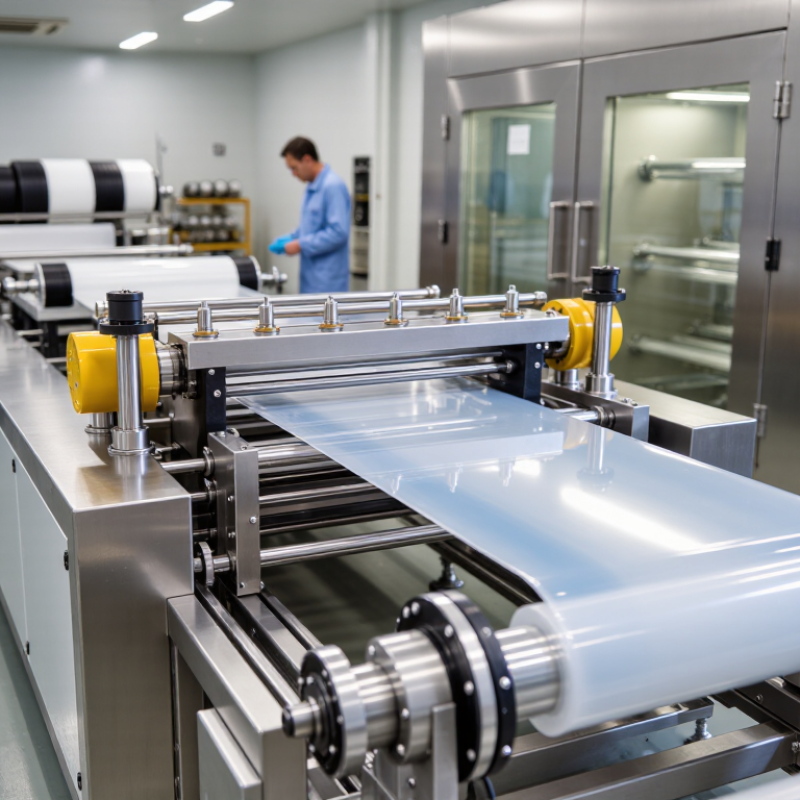
Define Slot Die Coating: 1–1,000 m/min Speed and 1–5,000 μm Wet Films
Top 10 China Slot Die Coating Machine Manufacturers?
Slot die coating is a precision process that meters liquid through a narrow die lip. It creates a controlled film on moving materials, including battery foils, films, and coated papers. In equipment specifications, speeds may range from 1 to 1,000 m/min. Wet-film thickness can range from 1 to 5,000 μm. These figures describe operating potential, not guaranteed production quality.
The International Energy Agency reported nearly 14 million electric car sales worldwide in 2023. This growth increases demand for accurate electrode and separator coating systems. At high speed, manufacturers must control pump pulsation, die-gap stability, web tension, and drying load. A 20 μm target can fail through a small pressure fluctuation. Clean edges matter.
Numbers need careful reading. A machine reaching 1,000 m/min may not handle a 5,000 μm wet film reliably. Viscosity, substrate roughness, coating width, and solvent behavior change the result. Smithers’ flexible-packaging market research also highlights continuing demand for efficient, material-saving coating technologies. However, brochures rarely show long-run defect rates. That is a weakness worth questioning.
For a practical comparison, buyers should request trial-coating records, thickness maps, startup waste data, and verified line-speed results. The best evaluation is not the largest number. It is repeatable performance under the buyer’s actual formula and substrate.
Top 10 China Slot Die Coating Machine Manufacturers? - Define Slot Die Coating: 1–1,000 m/min Speed and 1–5,000 μm Wet Films
Anonymous technical comparison of representative slot-die coating machine capability profiles commonly available from the Chinese industrial equipment market. The profiles are engineering reference ranges rather than a company ranking or a supplier certification.
Technical note: Actual operating limits depend on coating viscosity, rheology, solids content, die design, shim configuration, substrate surface energy, drying capacity, unwinding and rewinding equipment, and required coating uniformity. A slot-die coater meters the coating through a precision slot onto a continuously moving substrate; the practical wet-film range can extend from sub-micrometer layers to several millimeters in specialized applications.
Set Ranking Criteria: Web Width, Thickness Uniformity, Speed, and R&D Data
Top 10 China Slot Die Coating Machine Manufacturers?
A credible ranking should measure performance, not promotional language. Web width is a practical starting point. A 1.6-meter line may suit battery films, labels, or specialty coatings. However, usable width matters more than the advertised maximum. Check edge stability, coating access, and changeover time.
Thickness uniformity deserves the highest attention. Review cross-web deviation, longitudinal variation, and measurement methods. A strong machine should show repeatable results at different coating weights, not only one laboratory setting. Speed must be judged with quality. A line running at 80 meters per minute is less valuable when streaks, bubbles, or drying limits appear. I would compare stable production speed, acceleration behavior, and the actual coating window. Faster is not always better.
R&D data adds authority to the ranking. Look for pilot-line records, application trials, sensor calibration details, and documented improvements. Patent counts may help, but they do not prove useful engineering. Public data can also be incomplete. That weakness deserves disclosure. Tips: Request coated samples, raw uniformity charts, and a live trial using your own material. Ask how results change after several hours of continuous operation. Record temperature, viscosity, pump pressure, and line speed. Small details often expose large differences.
Profile China’s Top 10 Manufacturers by Products, Markets, and Certifications
Top 10 China Slot Die Coating Machine Manufacturers?
China’s leading ten slot die coating manufacturers serve lithium-ion batteries, adhesive films, optical films, separators, and flexible packaging. Their product ranges commonly include single-layer, multilayer, intermittent, and comma-assisted coating systems. Some also supply drying ovens, unwinding units, slurry tanks, and inline inspection equipment.
Market demand is substantial. The International Energy Agency reported that China represented about 60% of global electric car sales in 2023. That growth supports investment in battery electrode coating lines, where thickness control can affect yield and energy density. Industry reports from Smithers also identify flexible packaging and functional films as active coating markets. Yet, equipment rankings remain difficult. Public sales data is limited.
The strongest manufacturers usually target China, Southeast Asia, Europe, and North America. Their export packages may include CE documentation, ISO 9001 quality systems, and ISO 14001 environmental certification. These credentials matter, but certificates alone prove little. Buyers should inspect calibration records, coating uniformity data, factory acceptance tests, and after-sales response times. A practical benchmark is cross-web thickness variation below 3%, although material and speed change the result. Some suppliers advertise higher precision without publishing test conditions. That deserves caution. On-site trials with real slurry or adhesive are more reliable than brochures.
Compare Performance: ±1% Thickness Control, Automation, Yield, and Service
Top 10 China Slot Die Coating Machine Manufacturers: Comparing Performance
China’s slot die coating market serves batteries, films, adhesives, and specialty electronics. The International Energy Agency reported global battery demand above 750 GWh in 2023. That growth raises pressure on coating consistency and production yield. A serious comparison should verify ±1% thickness control across the full web width. It should not rely on a brochure claim.
The strongest machines combine closed-loop pumps, laser thickness sensors, and automatic gap adjustment. Check thickness data at startup, during speed changes, and after roll replacement. Stable control matters more than impressive peak speed. The International Federation of Robotics recorded 541,302 industrial robot installations worldwide in 2023. This supports wider use of automated loading, recipe control, inspection, and defect tracking. Still, automation can repeat a bad setting perfectly. Human process review remains necessary.
Yield depends on more than coating accuracy. Ask for first-pass yield, material waste, uptime, changeover time, and cleaning hours. Request trial-coated samples using your actual slurry and substrate. Service quality also needs measurable evidence. Review spare-parts availability, remote diagnostics, technician response time, and software update procedures. A useful acceptance test should define thickness deviation, coating streak limits, web tension stability, and recovery after an emergency stop. Some suppliers may achieve ±1% under ideal laboratory conditions, yet struggle with foaming, edge beads, or unstable viscosity. That gap deserves attention. Perfect claims are rarely perfect.
Evaluate Demand in Batteries, Displays, Solar Cells, and Functional Films
Selecting among the top 10 China slot die coating machine manufacturers requires more than comparing machine prices. Battery production demands stable slurry delivery, accurate coating weight, and clean operation. A practical evaluation should examine slot-die gap control, pump response, web tension, drying integration, and changeover time. Small coating errors can affect electrode capacity and production yield.
Display films need exceptional uniformity across wide, delicate substrates. Ask manufacturers for measured thickness variation, defect inspection methods, and sample results from pilot trials.
Solar cell production often prioritizes high throughput, low material waste, and reliable operation over long shifts. Functional films may require multilayer coating, narrow patterns, or water-based formulations. The machine must handle these differences without forcing one standard setup.
Real experience matters. Request a factory demonstration using your actual slurry, substrate, and target speed. Review maintenance records, calibration procedures, operator training, and spare-part availability. I would not trust impressive brochures alone. No machine wins every application. Some suppliers may show excellent laboratory results but struggle with continuous production. This is where evaluation becomes uncomfortable. A slower line with stable quality may outperform a faster line with frequent cleaning and rejects. Engineers should record coating weight, edge quality, downtime, and waste during repeated trials, not only during a carefully prepared demonstration.